What Is an HDD SATA Board?
An HDD SATA board is the electronic controller PCB installed on the underside of a mechanical Serial ATA hard disk drive. It connects the drive to a computer and controls communication between the computer and the drive’s internal mechanical systems.
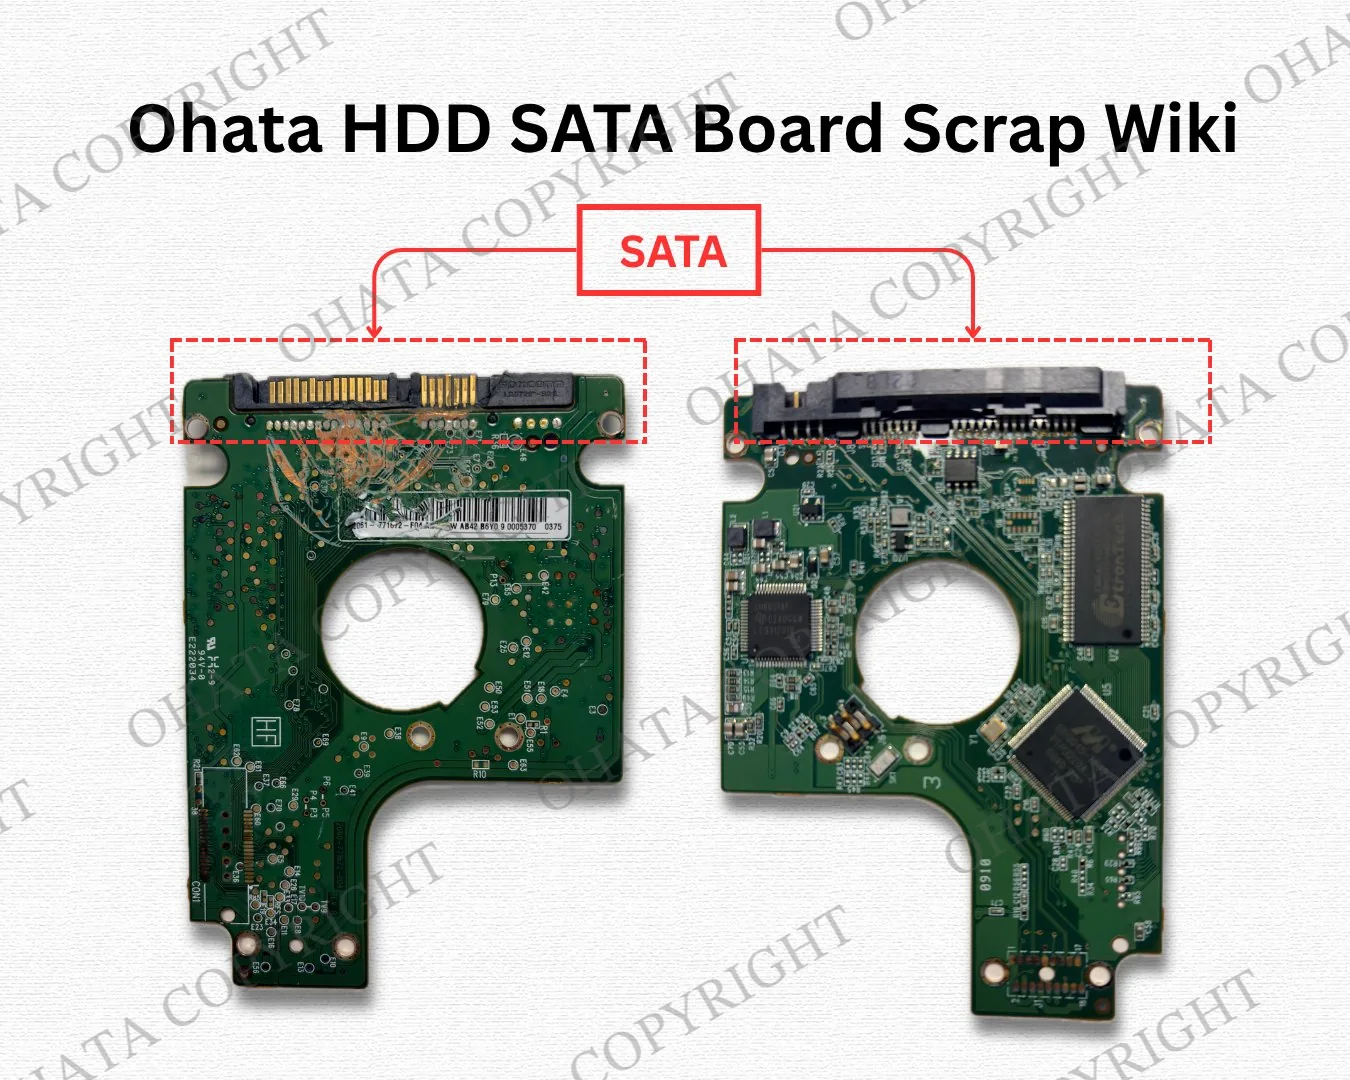
The board works with the spindle motor, actuator arm, read/write heads, magnetic platters, and internal sensors. It also manages firmware, cache memory, power distribution, error correction, and drive-health monitoring.
Commands to read, write, diagnose, or monitor the hard drive pass through the controller board before reaching the magnetic storage system. Without its matching controller board, a mechanical hard drive normally cannot operate or communicate correctly.
This guide covers controller boards removed from mechanical SATA hard drives. It does not cover SSD boards, USB bridge adapters, optical-drive controllers, SAS boards, or other non-SATA drive boards.
What Does an HDD SATA Board Control?
The HDD SATA board acts as the electronic management system for the complete hard drive. It translates commands from the computer into the electrical signals required to operate the drive.
Its main functions include:
managing SATA communication with the computer
starting and regulating the spindle motor
positioning the actuator and read/write heads
processing data read from or written to the platters
executing drive firmware
managing cache or buffer memory
performing error correction
monitoring SMART health information
regulating and distributing electrical power
protecting components from unsuitable voltage or current conditions
The board is designed specifically for the drive family in which it was installed. Even boards with similar physical shapes or connector arrangements may use different firmware, calibration information, or electrical designs.
History of SATA Hard Drives
Mechanical hard drives have been used for computer storage for decades. Early drives were large and expensive, but they became smaller and more affordable as personal computers expanded during the 1980s and 1990s.
Many drives from the 1990s used the Integrated Drive Electronics interface, commonly called IDE and later standardized as Parallel ATA or PATA. These drives connected through wide ribbon cables and transferred several data bits in parallel.
Serial ATA was introduced in the early 2000s. SATA replaced wide parallel connections with smaller serial data and power connectors. The interface simplified installation, improved airflow within computer enclosures, supported higher transfer rates, and provided more reliable high-speed communication.
Three major SATA generations were introduced:
SATA I: 1.5 Gb/s
SATA II: 3.0 Gb/s
SATA III: 6.0 Gb/s
The SATA generation describes the interface’s nominal performance. It does not determine the recycling category or purchasing value. A newer or faster controller board is not automatically more valuable as scrap.
Although SSDs have become common, mechanical SATA drives remain in use because they can provide substantial storage capacity at a lower cost per unit of storage. Large numbers of these drives continue to enter the recycling stream.
Where Are HDD SATA Boards Found?
Desktop computers commonly use 3.5-inch SATA hard drives for operating systems, software, and data storage. Laptop computers produced before the widespread adoption of SSDs frequently use smaller 2.5-inch SATA drives.
External hard-drive enclosures may contain standard SATA drives connected to a separate USB bridge board. Once the drive is dismantled, the PCB attached directly to the mechanical hard drive is the HDD SATA board. The separate USB adapter is not part of this category.
Servers and network-attached storage systems may contain several SATA drives operating together in a storage array. DVR and NVR surveillance systems also use SATA drives for continuous video recording.
Other possible sources include industrial computers, manufacturing equipment, laboratory systems, embedded controls, backup devices, and gaming systems.
The equipment in which a drive was used can support identification, but it does not determine the controller board’s purchasing category by itself.
HDD SATA Board Construction
HDD SATA boards are commonly produced from multilayer fiberglass-reinforced epoxy laminate, generally known as FR-4. Copper layers inside the PCB provide signal routing, grounding, and power distribution.
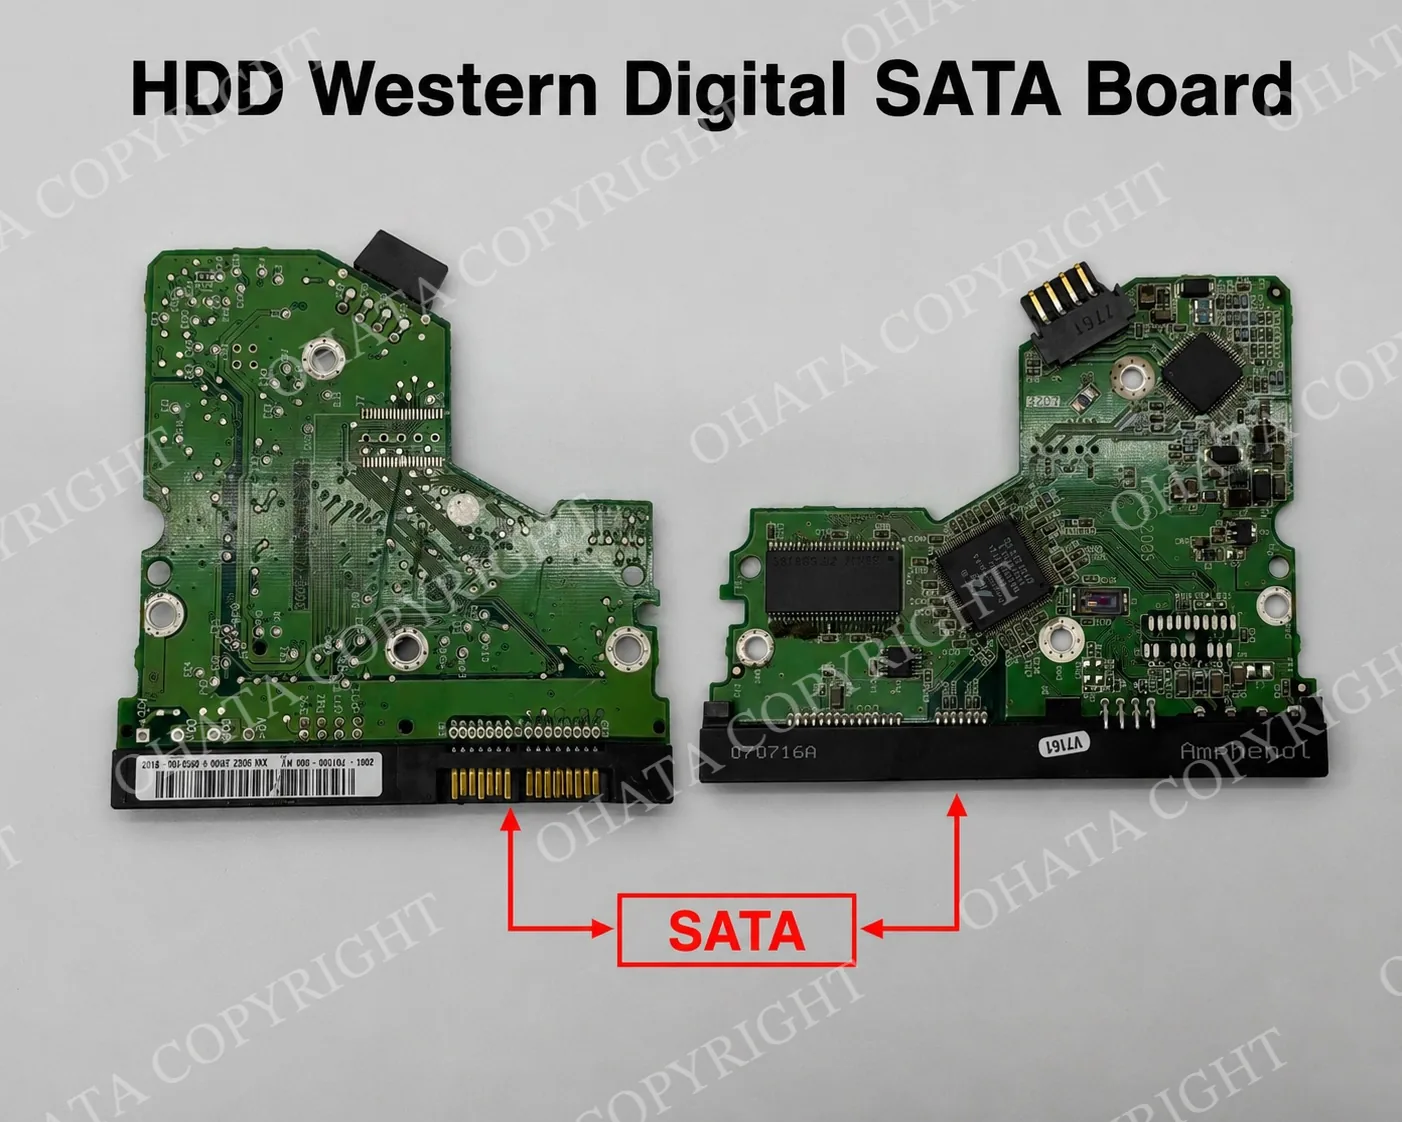
The exterior normally contains a protective solder mask, printed component markings, contact pads, mounting holes, and surface-mounted components. Most boards are green, although black, blue, and other solder-mask colors may also be found.
Unlike a rectangular desktop motherboard, an HDD controller board usually has an irregular outline designed to fit a particular hard-drive housing. Its mounting holes, connector edge, and internal contact areas must align with the drive’s mechanical structure.
Common construction features include:
multilayer copper circuitry
surface-mounted integrated circuits
a protective solder mask
printed part numbers and component markings
SATA data and power connectors
internal motor and head contacts
test points and grounding areas
mounting holes for attachment to the drive
PCB manufacturing generally involves multilayer fabrication, copper-pattern formation, drilling, through-hole plating, solder-mask and silkscreen application, surface finishing, automated component placement, reflow soldering, optical inspection, and electrical testing.
Exact materials, layouts, and manufacturing methods vary by manufacturer, model, and production period.
How to Identify an HDD SATA Board
The fastest visual check is the connector edge. A standard SATA hard-drive board has a narrow 7-pin data connection beside a wider 15-pin power connection. Both use a recognizable keyed, L-shaped design.
After confirming the SATA connector pair, inspect the complete board:
Inspection point
What to examine
Original application
Controller board removed from a mechanical hard disk drive
SATA interface
Adjacent 7-pin data and 15-pin power connections
Main controller
Usually one of the largest integrated circuits on the board
Motor control
Motor-driver circuitry connected to the spindle and actuator
Memory and firmware
Cache memory and a separate ROM or flash chip where used
Power circuitry
Regulators, MOSFETs, inductors, capacitors, and protection devices
Internal contacts
Contact areas connecting the board to the drive mechanism
PCB construction
Compact, irregular outline with mounting holes
Completeness
Original chips, connectors, contacts, and PCB sections
Condition
Corrosion, burning, liquid exposure, breakage, or harvesting
The component side generally provides the clearest identification features. It commonly contains the controller IC, cache memory, motor driver, voltage-regulation circuitry, manufacturer markings, and SATA connectors.
The reverse side may contain fewer components, but it remains important during inspection. It can show internal drive contacts, test points, grounding areas, revision codes, manufacturing numbers, solder joints, and damage not visible from the front.
Both sides should be inspected. The SATA connector pair is the strongest initial clue, but it does not replace examination of the complete board.
Major Electronic Components
The main controller IC, sometimes called the controller ASIC, manages SATA communication, firmware execution, data processing, error correction, cache operation, drive initialization, SMART monitoring, and read/write control.
It is commonly one of the largest square or rectangular packages on the PCB. Depending on the design, it may use a BGA or another fine-pitch surface-mount package. Marvell, Broadcom, LSI, and hard-drive manufacturers have produced controller devices for different drive families.
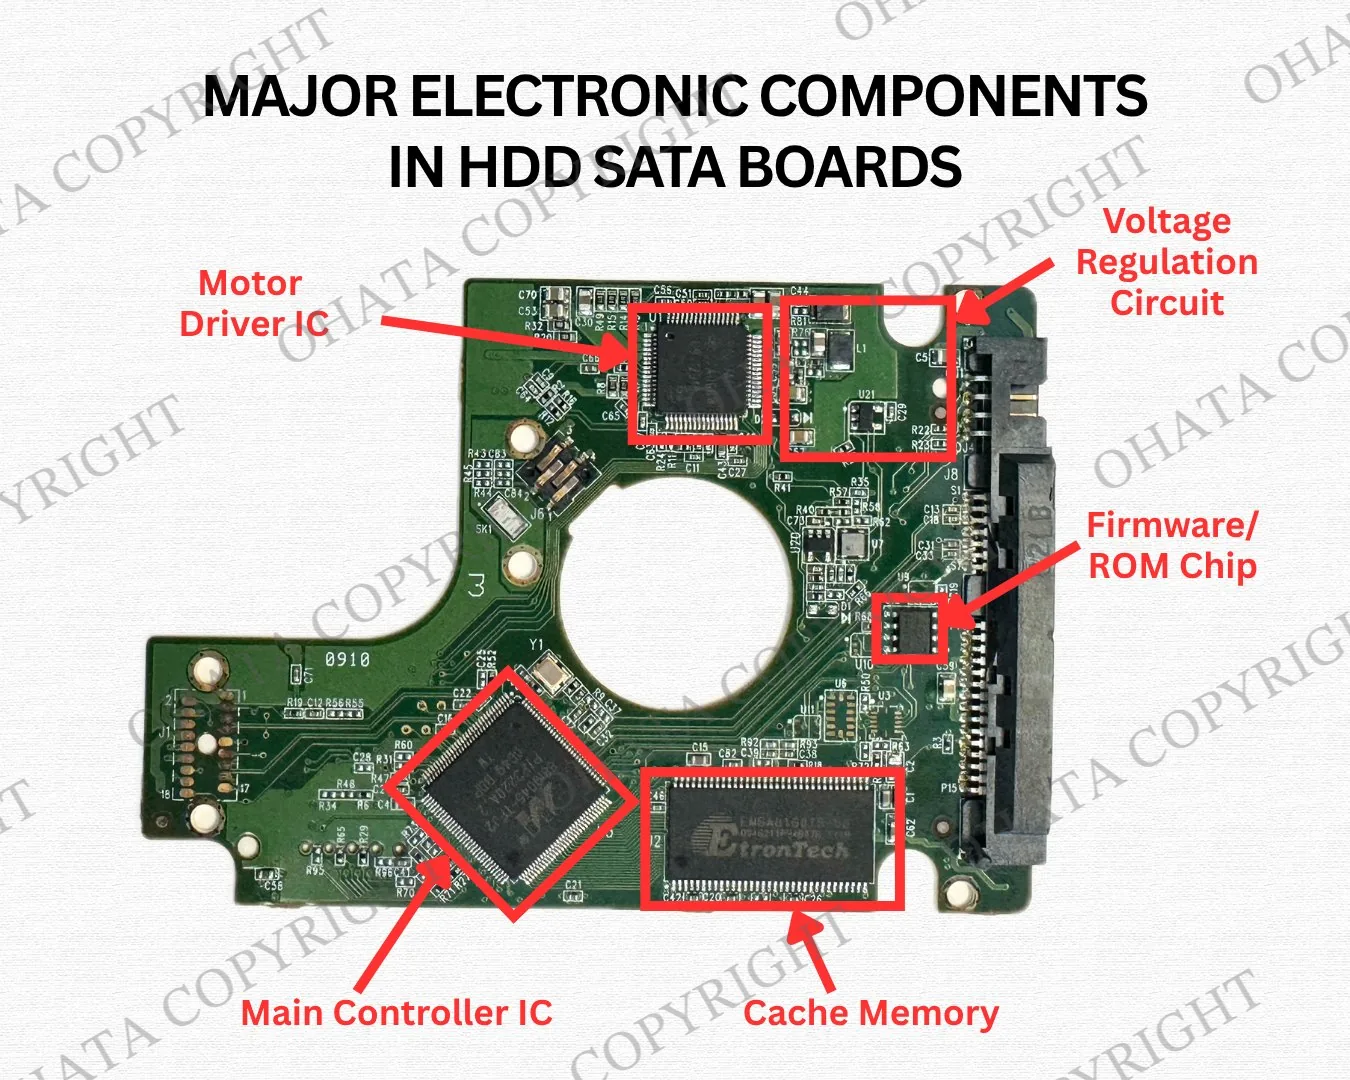
Cache memory, also called buffer memory, temporarily stores data during read and write operations. It is generally positioned close to the main controller. Older consumer drives may have relatively small caches, while newer consumer or enterprise drives may use 256 MB or more.
The motor-driver IC supplies and controls power for the spindle motor and voice-coil actuator. It starts and maintains platter rotation, positions the read/write heads, manages acceleration and braking, and monitors motor operation.
Because the motor driver handles greater electrical current than many logic components, it may be positioned close to the internal motor contacts and connected through wider copper pathways.
Some boards have a separate firmware or ROM chip containing startup instructions, factory calibration values, adaptive parameters, and hardware-configuration information associated with the drive. When present, it is often a small eight-pin surface-mounted package near the controller.
Other designs integrate firmware functions into the controller IC. The absence of a separate ROM package does not automatically mean that a component has been removed.
Power Regulation and Passive Components
Power arriving through the SATA power connection must be converted into stable voltages before it reaches the controller, cache memory, motor driver, and other sensitive components.
The voltage-regulation and protection area may contain regulators, MOSFETs, inductors, ceramic or electrolytic capacitors, diodes, current-sensing resistors, and electrical filters.
This circuitry performs several functions, including voltage conversion, current regulation, noise suppression, reverse-polarity protection, overvoltage protection, and stable power distribution.
Numerous smaller resistors, capacitors, oscillators, ferrite beads, and filters support signal stability, timing, power filtering, and reliable operation.
Component placement and chip count vary. Manufacturers may combine several functions within one IC, so qualifying HDD SATA boards will not all have the same number or arrangement of visible components.
SATA Connectors and Internal Drive Contacts
Every standard SATA HDD board uses a 7-pin data connector and a 15-pin power connector. The data connector carries information between the drive and host system, while the power connector supplies the voltages required by the controller board and spindle motor.
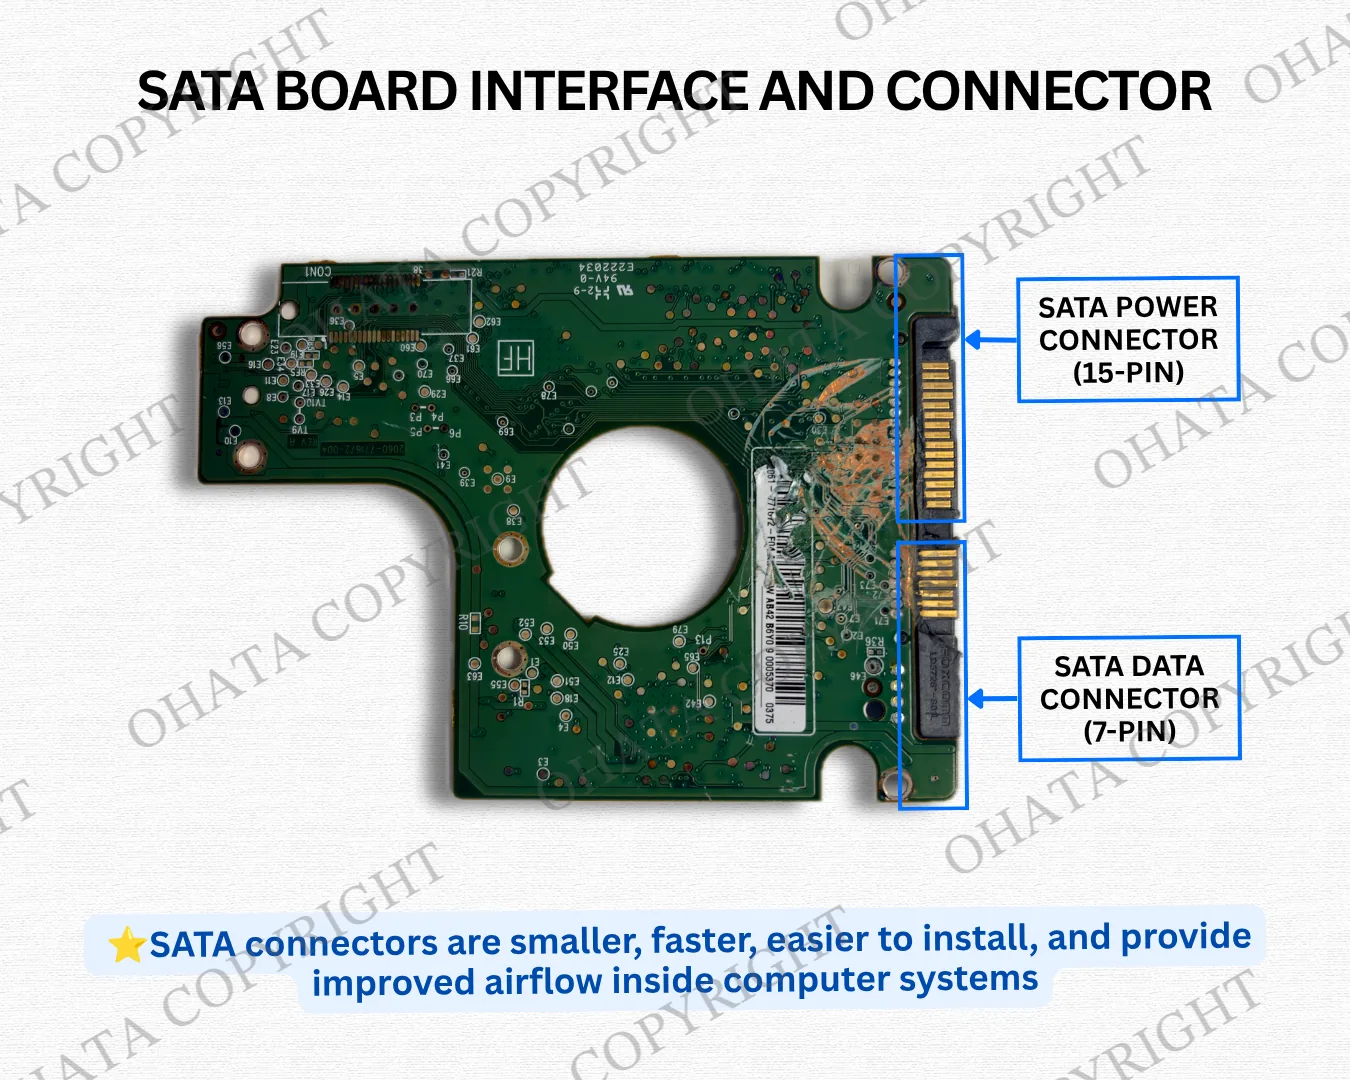
The connectors are smaller than older IDE ribbon-cable systems and use a keyed shape that helps prevent incorrect insertion. Selected contact surfaces may use a thin gold finish to improve corrosion resistance and electrical reliability.
The quantity of gold on these contacts is very small. Their importance for identification is greater than their visible size or appearance might suggest.
The board also contains contacts that connect to the hard drive’s internal spindle motor and read/write head assembly. These commonly align with spring-loaded contacts when the controller board is attached to the drive housing.
Internal contacts can be found on the component side or reverse side depending on the board design. Missing, cut, heavily corroded, or damaged contact areas may affect completeness and purchasing value.
Common Manufacturers and Board Designs
Western Digital, Seagate, Toshiba, Hitachi or HGST, Samsung, and Fujitsu have produced mechanical SATA hard drives. Each manufacturer has used multiple controller designs across different drive sizes, models, and production periods.
Western Digital boards often use compact, model-specific layouts. Seagate boards are common in consumer, enterprise, and surveillance equipment. Toshiba boards are frequently found in laptops, desktops, and other systems.
Hitachi and HGST produced consumer and enterprise drives. Samsung manufactured mechanical SATA drives before shifting its storage focus primarily toward solid-state products. Fujitsu produced drives for notebook and business systems.
Manufacturer names, logos, printed numbers, labels, revision codes, and PCB shapes can support identification. However, manufacturers may use several board revisions within the same period.
A printed year does not always establish the exact production category. Likewise, two boards from the same manufacturer may require different purchasing categories because of differences in size, design, components, or manufacturing period.
Manufacturer and date markings should be considered with the complete board rather than used as the only classification evidence.
Recoverable Materials and Recycling Value
Although smaller than a computer motherboard, an HDD SATA board contains recoverable electronic material concentrated within a compact PCB.
Copper commonly represents a substantial part of the recoverable metal by weight. It is present in internal layers, surface traces, ground planes, power-distribution areas, contact pads, through-hole plating, component leads, and other conductive pathways.
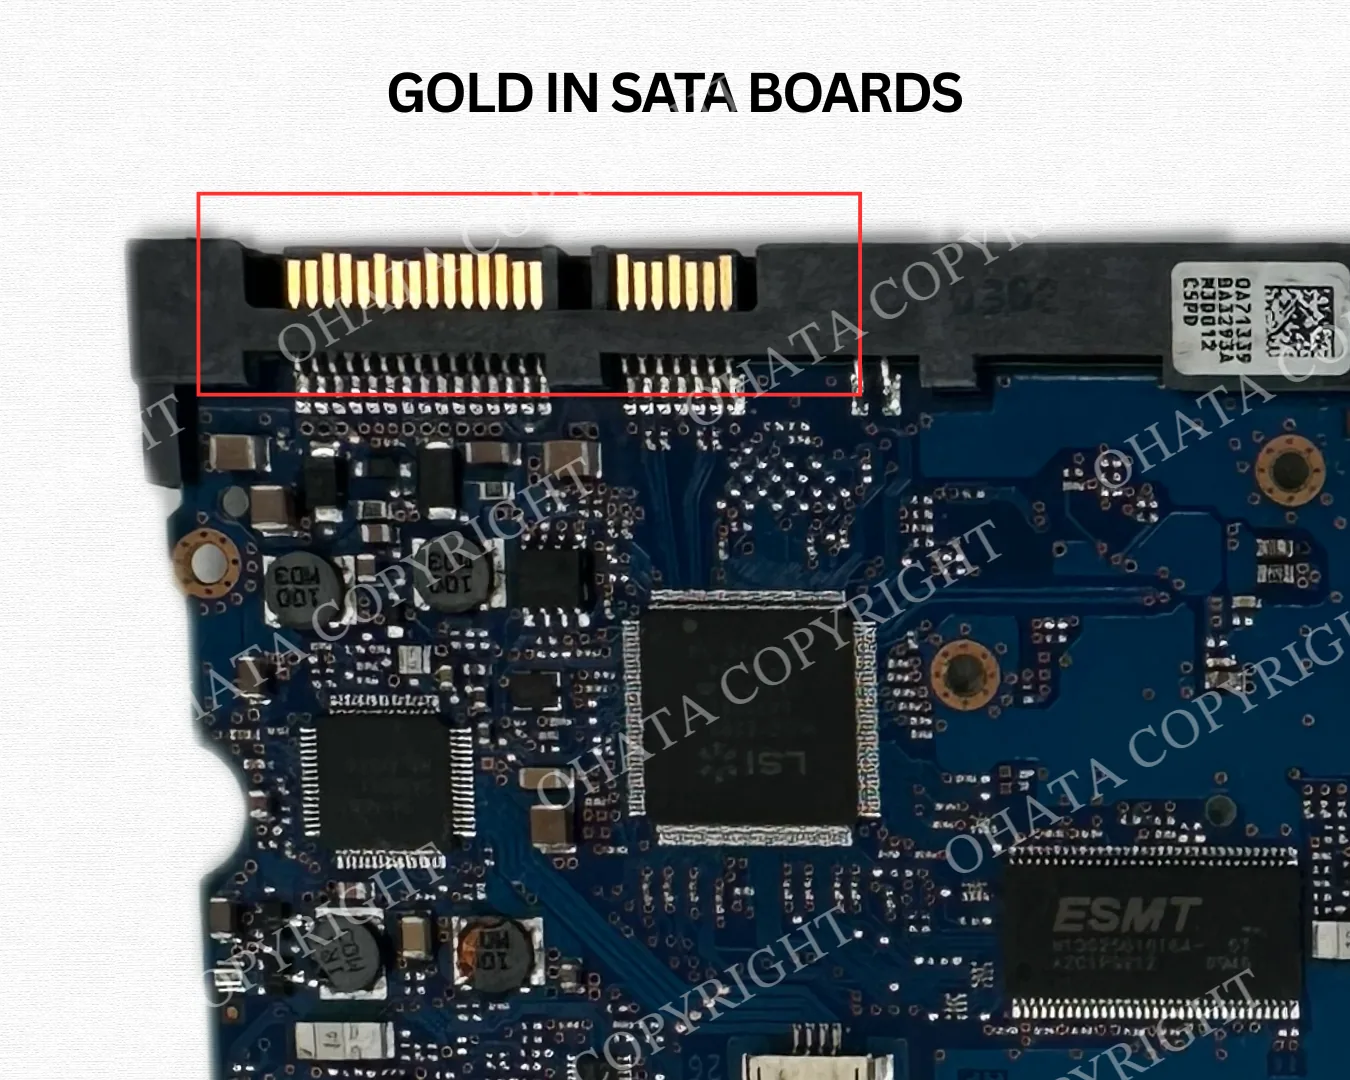
Gold may be present as a thin surface finish on selected SATA contacts, internal drive contacts, test pads, and certain electronic components. Tin is commonly associated with solder, while nickel may be used beneath connector finishes or within other metal structures.
Silver may be present in certain solder alloys or electronic components. Palladium may occur in some components depending on their materials and manufacturing period, but it should not be assumed to be present in a specific quantity without representative laboratory analysis.
Limited aluminum, steel, silicon-based semiconductor material, fiberglass, and resin may also be present.
The exact composition varies by manufacturer, model, production period, PCB construction, and component supplier. A photograph cannot determine internal copper weight, plating thickness, solder composition, or precious-metal quantity.
One large IC or gold-colored connector does not determine the board’s value. Evaluation considers the complete component population, construction, retained contacts, physical condition, contamination, and processing requirements.
Professional recovery may involve mechanical preparation, metal separation, smelting, hydrometallurgical treatment, or other controlled refining processes.
Recycling these boards helps recover copper and other usable materials, reduces electronic waste sent to disposal, and decreases the need for newly mined material.
Do not burn boards, scrape contacts, cut plated sections, grind components, or apply chemicals to test for metals. These actions can reduce recoverable value and create fire, dust, chemical, and environmental hazards.
SATA and Non-SATA HDD Boards
SATA and non-SATA are broad identification groups used to distinguish hard-drive controller boards by interface. Current buying categories may divide boards further by manufacturer, drive size, design, or production period.
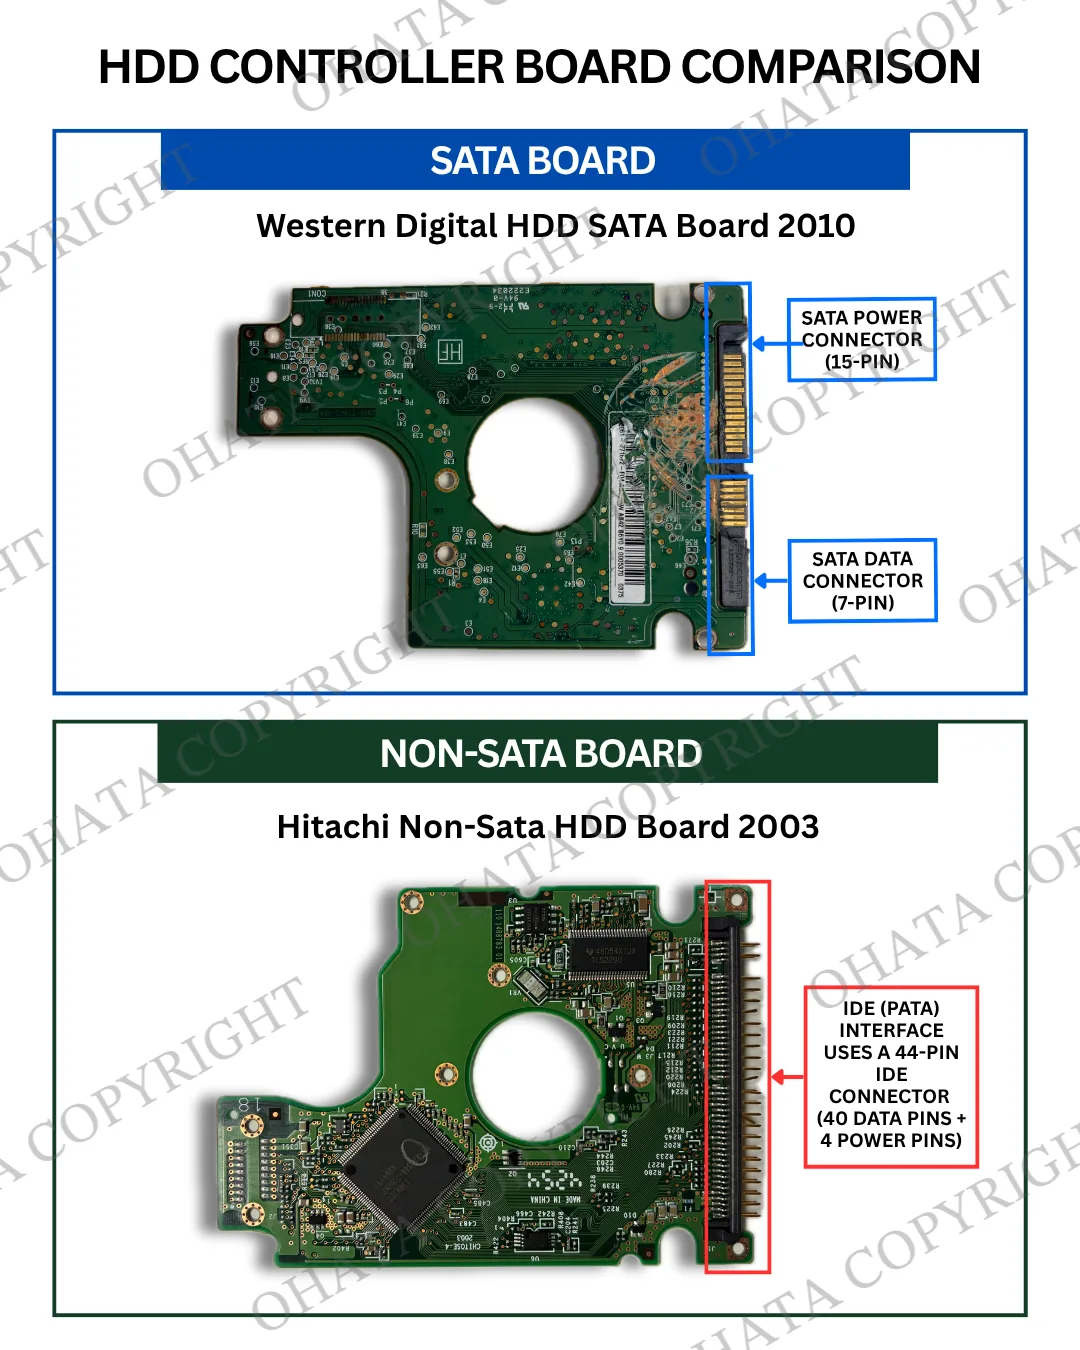
A SATA HDD board uses the standard 7-pin data and 15-pin power connector pair. These boards became common from the early 2000s onward.
Non-SATA HDD boards may use IDE, PATA, ATA, EIDE, SCSI, or another legacy or proprietary interface. They commonly have wide pin headers, ribbon-cable connections, or larger connector systems instead of the standard SATA pair.
The interface type is the primary distinction between these broad groups. It should not be assumed that every board within one group receives the same purchasing price.
Learn more about HDD Non-SATA Board Scrap.
Learn more on YouTube: How to Identify SATA and Non SATA HDD Boards
Boards Commonly Confused With HDD SATA Boards
SSD boards contain NAND flash-memory packages and do not control a spindle motor, actuator, or mechanical read/write heads. They belong to a separate category even when their device uses a SATA connection.
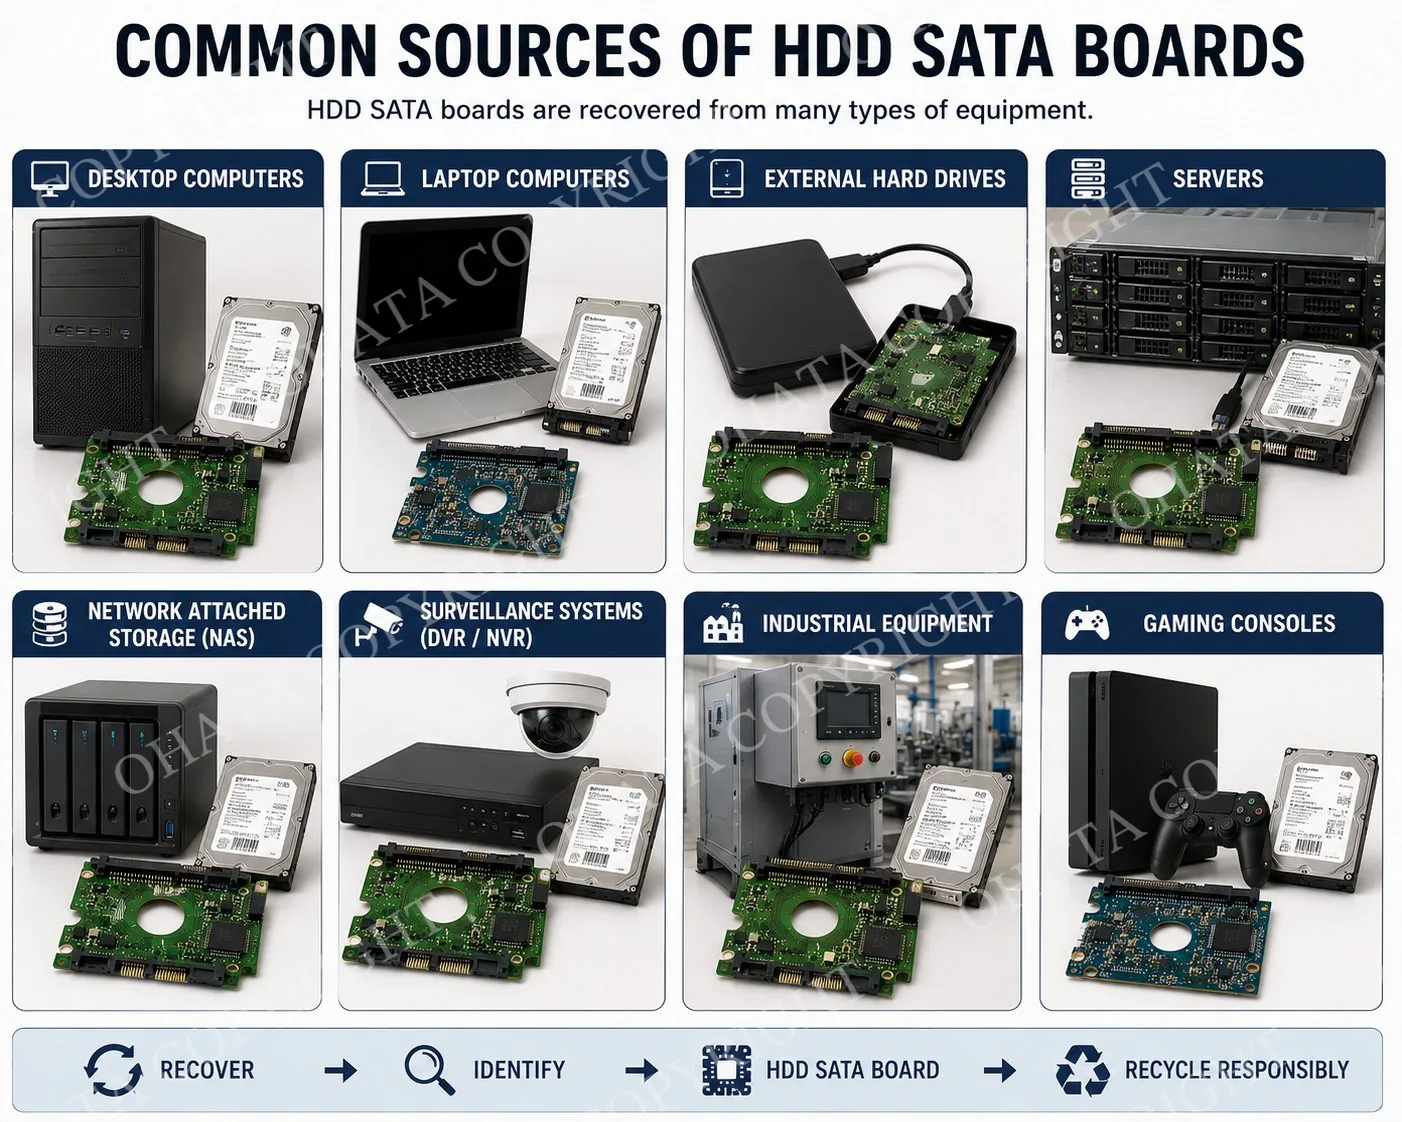
USB bridge boards convert SATA communication to USB within some external-drive enclosures. The bridge board is separate from the controller PCB attached directly to the mechanical hard drive.
Optical-drive controller boards operate CD, DVD, or Blu-ray mechanisms. They may contain motor-control circuitry but use different connector arrangements and mechanical interfaces.
Laptop logic boards are generally larger and contain the main computer processor, memory connections, display connections, USB ports, and broader system-control circuitry.
Appliance boards commonly use relays, transformers, larger power components, and connectors intended for household equipment. Their construction and original function differ from HDD controller boards.
SAS and other enterprise-drive boards may use connector systems resembling SATA but belong to different interface or purchasing categories.
Correct identification depends on the complete combination of the SATA connector pair, original mechanical-drive application, controller IC, motor-driver circuitry, internal contacts, and PCB shape.
Complete, Incomplete, and Damaged Boards
A complete HDD SATA board retains its original PCB structure and major factory-installed components. The controller IC, motor driver, cache memory where used, separate firmware chip where applicable, voltage-regulation circuitry, connectors, and internal contacts should remain present.
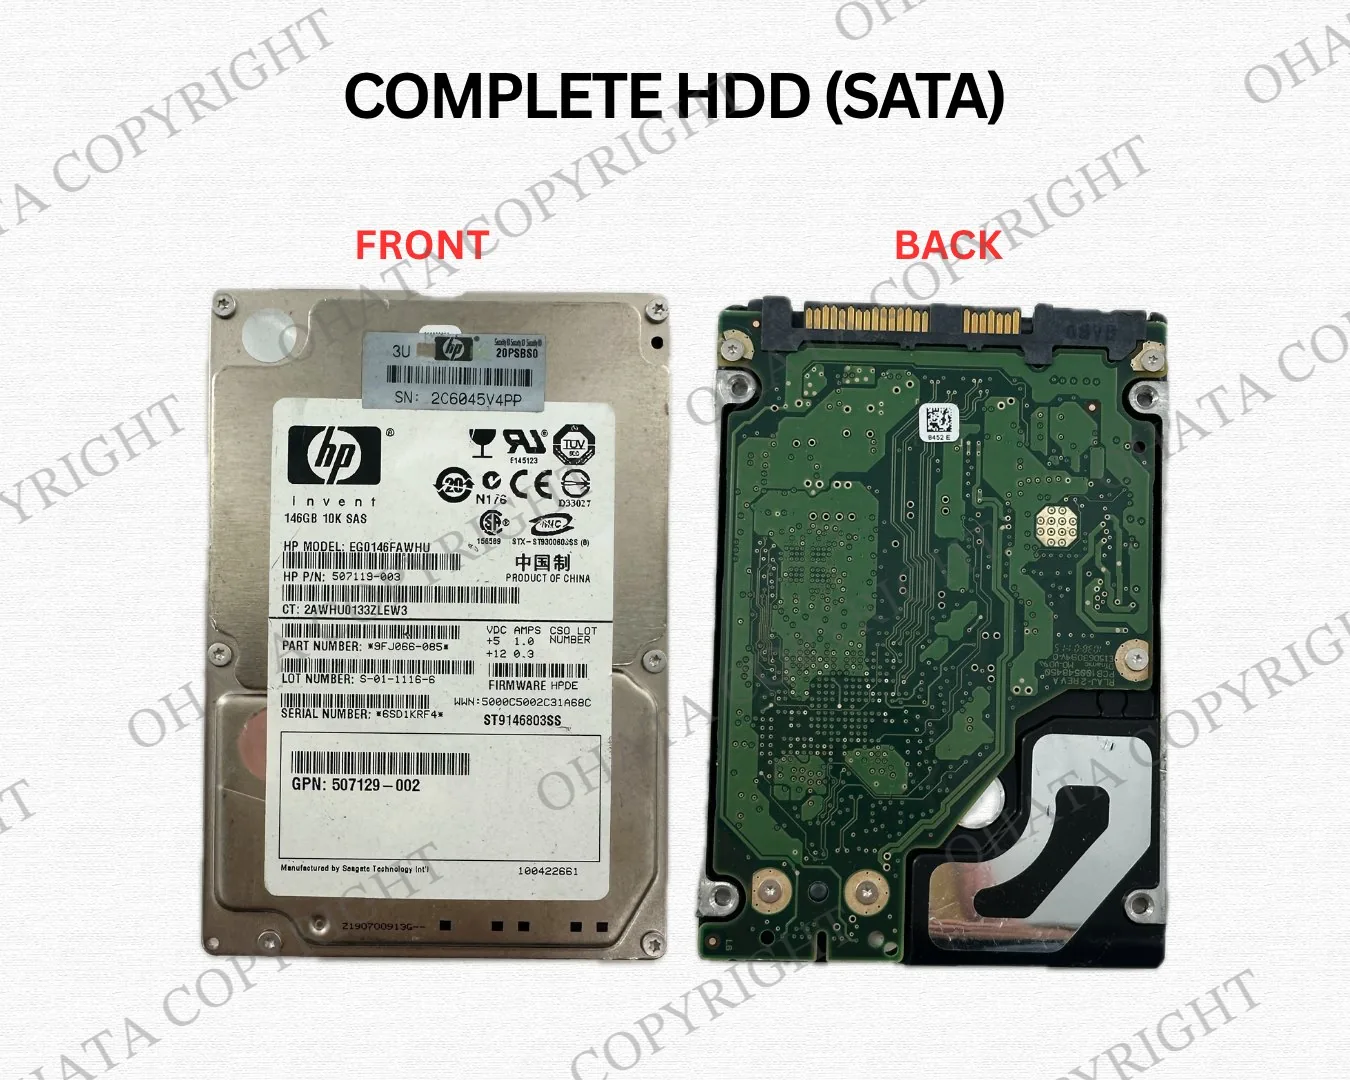
An incomplete board may have removed semiconductor packages, missing connectors, broken contact areas, cut sections, cracks, drilled holes, or extensive component harvesting.
Missing removable or separately designed components should be judged according to the original board design. For example, a board without a separate ROM chip may still be complete if its firmware function was integrated into the controller.
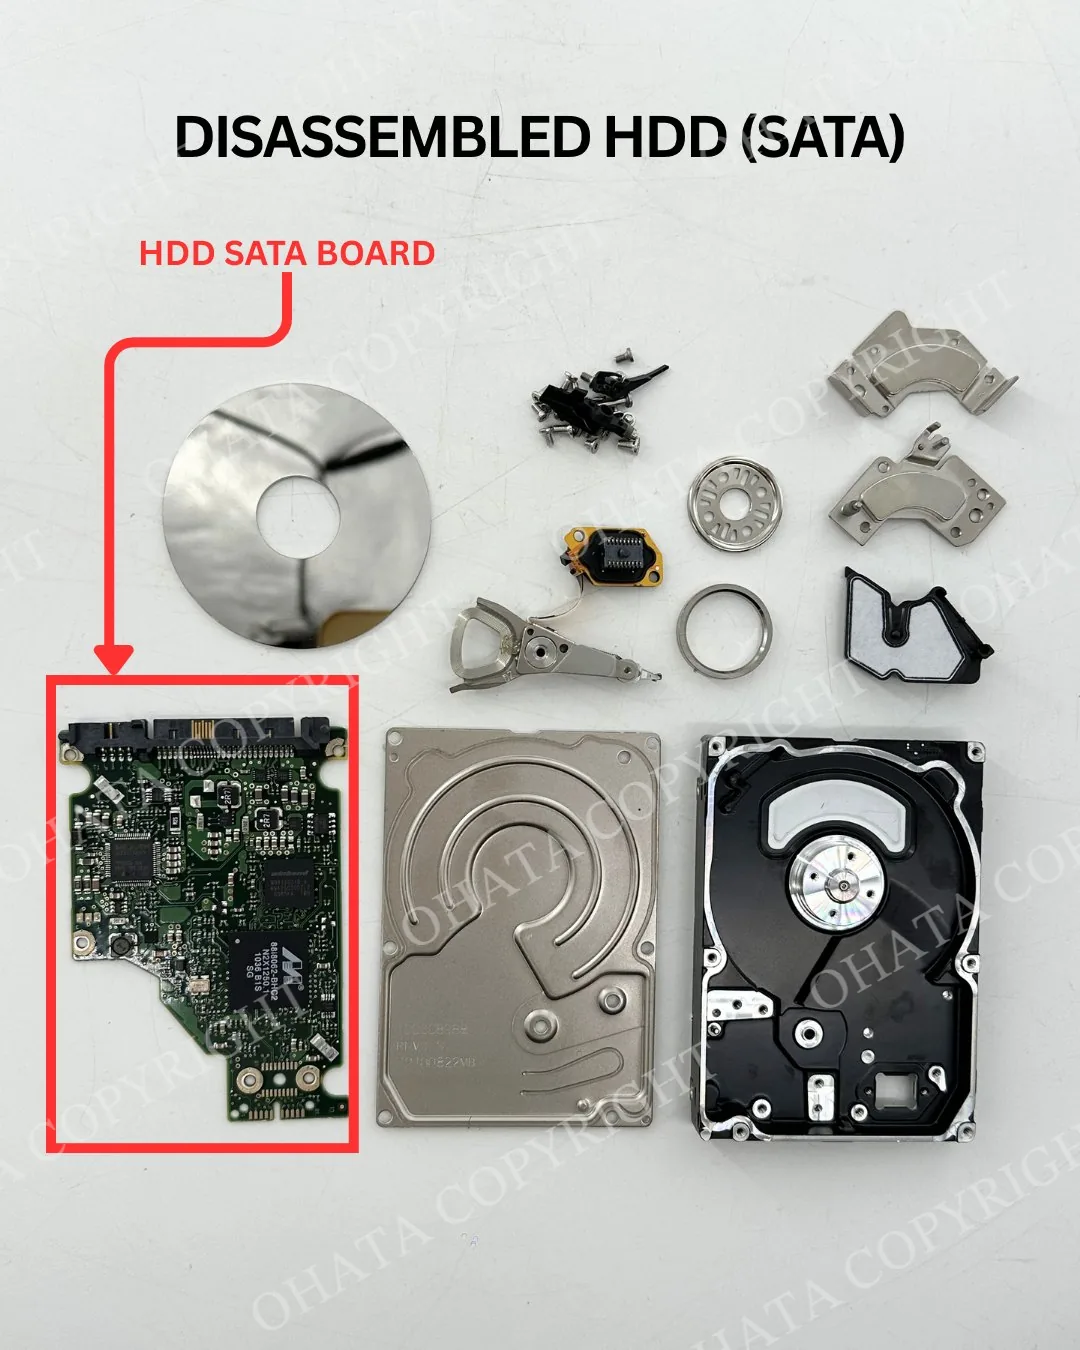
Damage may result from electrical faults, power surges, overheating, moisture exposure, mishandling, repair attempts, or intentional destruction.
Common conditions include:
burned or discolored power circuitry
corrosion on connectors, contacts, or solder joints
cracked fiberglass and broken corners
damaged mounting holes or connector housings
heat-discolored solder mask
missing chips or empty solder-pad areas
cut, bent, drilled, or fragmented PCBs
A damaged board may remain identifiable as an HDD SATA board when sufficient original construction is present. However, damage can still affect acceptance, classification, or purchasing value.
Sorting and Buying Guidelines
Purchases of qualifying HDD SATA controller-board scrap start at 1 lb. The boards do not need to function because evaluation is based on physical construction and recoverable material rather than electronic performance.
For the best evaluation:
keep the controller, motor driver, memory, firmware components, power circuitry, and connectors attached
keep the boards dry and reasonably clean
inspect and protect both sides
separate SATA boards from non-SATA and SSD boards
separate manufacturers, designs, sizes, and production categories when required
keep complete hard drives separate from loose controller boards
remove unrelated plastic, loose metal, wires, batteries, and packaging
protect boards from unnecessary bending or breakage
Normal labels, handling marks, light dust, and minor surface wear may be acceptable when the board remains substantially complete and identifiable.
Boards with removed chips, missing connectors, broken sections, corrosion, water damage, burning, or substantial contamination may receive a different classification or reduced purchasing value.
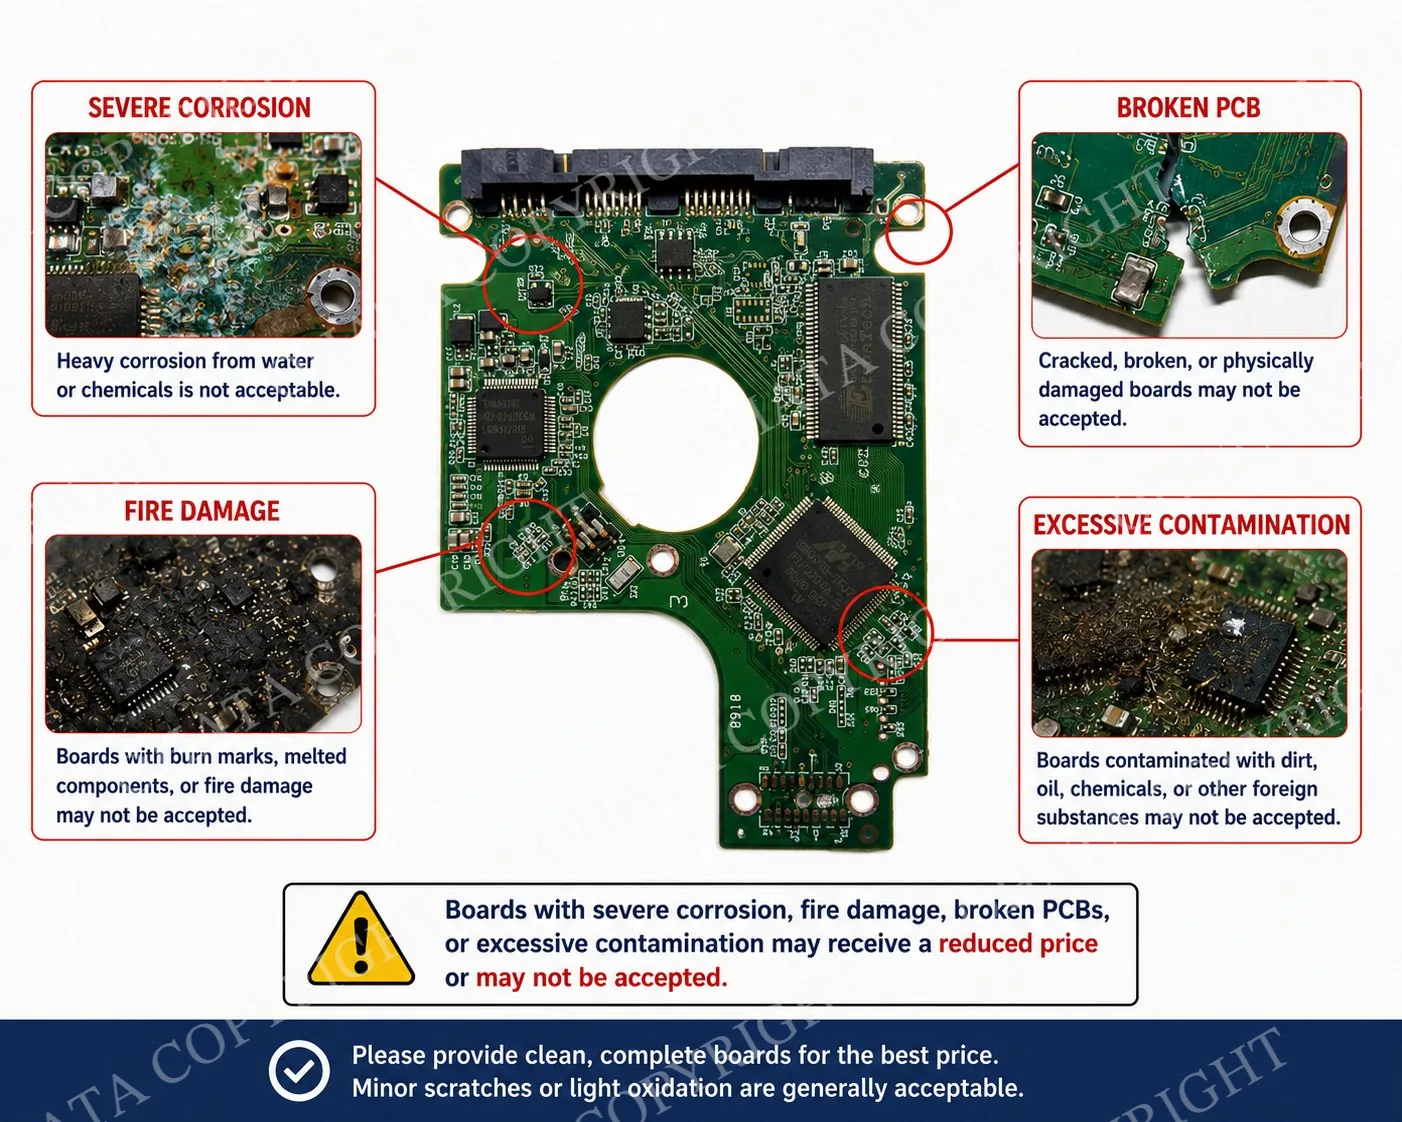
Severely burned, carbonized, chemically treated, hazardous, extensively fragmented, or unidentifiable material may be rejected after inspection.
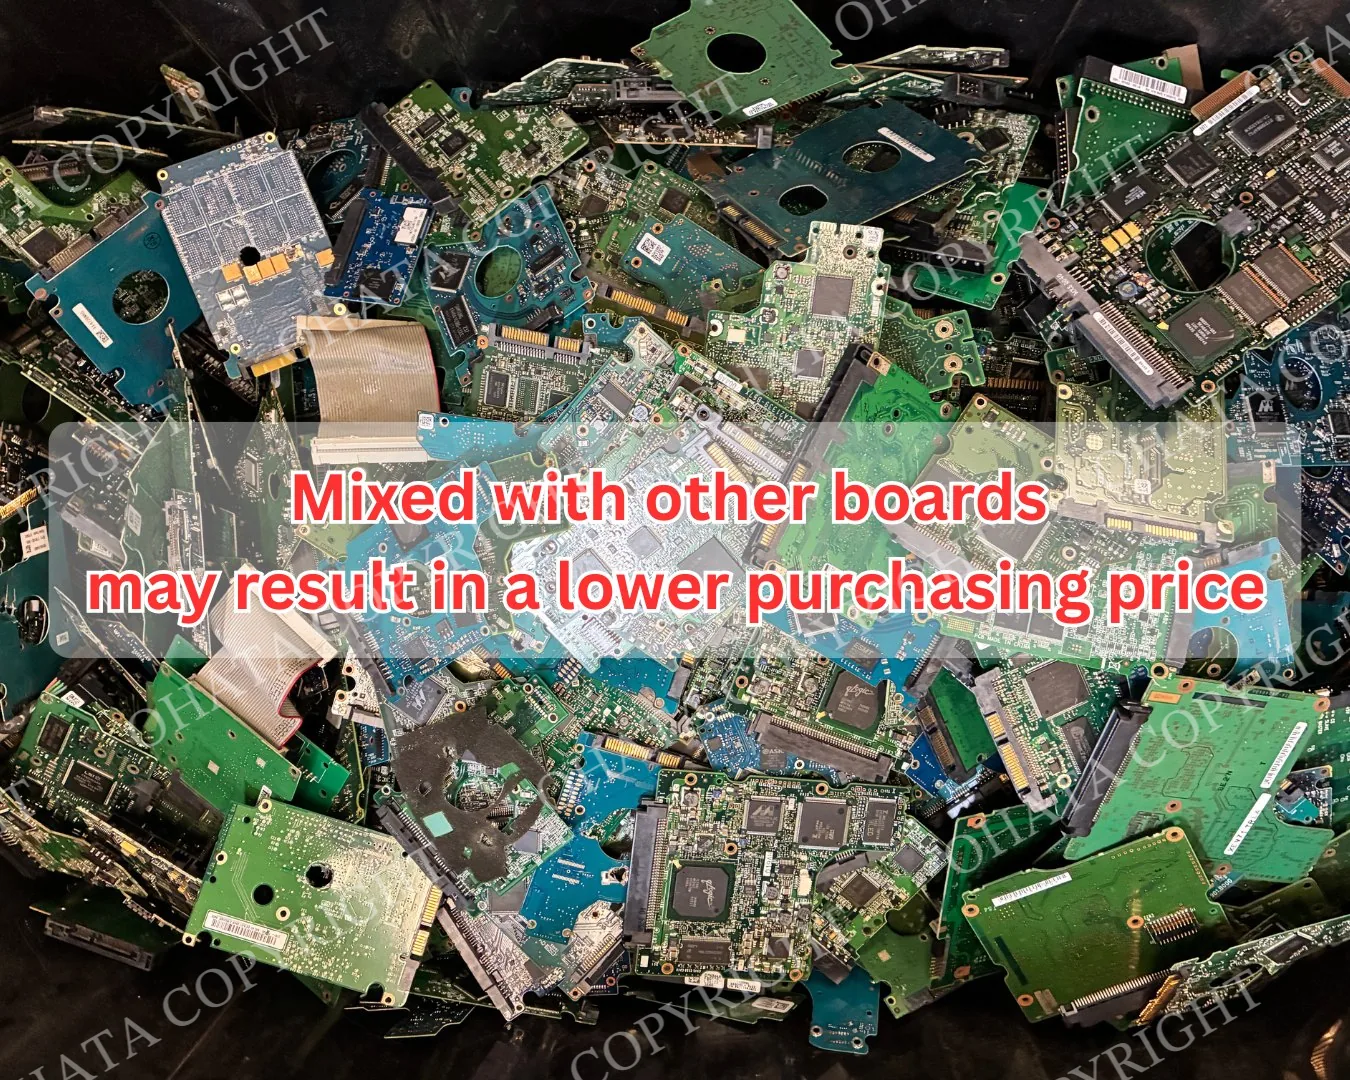
Mixed material may require separate inspection, sorting, weighing, and pricing. A mixed group should not be assumed to receive one uniform price.
Data and Storage Considerations
A loose HDD controller board normally does not contain the user documents, photographs, or other files stored on the hard drive. These files are generally recorded magnetically on the platters inside the drive enclosure.
However, the controller board may contain firmware and drive-specific calibration information. This information supports operation of the drive but is different from the ordinary user files stored on its platters.
Complete data-bearing drives should be handled according to appropriate data-security procedures. Sellers remain responsible for protecting or removing their information before the device changes ownership.
Physical removal of the controller board alone is not a reliable method of permanently erasing information from the magnetic platters.
Current Buying Price and Classification
Current purchasing categories may identify HDD SATA boards according to their manufacturer, drive size, PCB design, and approximate production period.
As of September 3, 2026, qualifying Western Digital 2005 HDD SATA boards and Seagate 3.5-inch 2007 HDD SATA boards are each listed at $10.80 USD per lb for the Seattle buying location.
These are item-specific purchasing categories. Their prices should not be interpreted as one guaranteed price for every SATA controller board.
Storage capacity, rotational speed, SATA generation, firmware version, original retail price, and working condition do not determine the category by themselves. Classification considers the manufacturer, board design, component population, completeness, physical condition, contamination, and current purchasing requirements.
Prices and conditions may change with material markets and processing requirements. The applicable buying page should be checked before sorting or selling material.
The Ohata HDD Classification is an independent purchasing, sorting, identification, and recycling system. It is not a government regulation, ISO specification, storage-performance rating, or universal electronic-scrap standard.
Final classification, acceptance, and purchasing value are confirmed after inspection under current buying requirements.